Hydroquinone – High Purity Pharmaceutical Raw Material
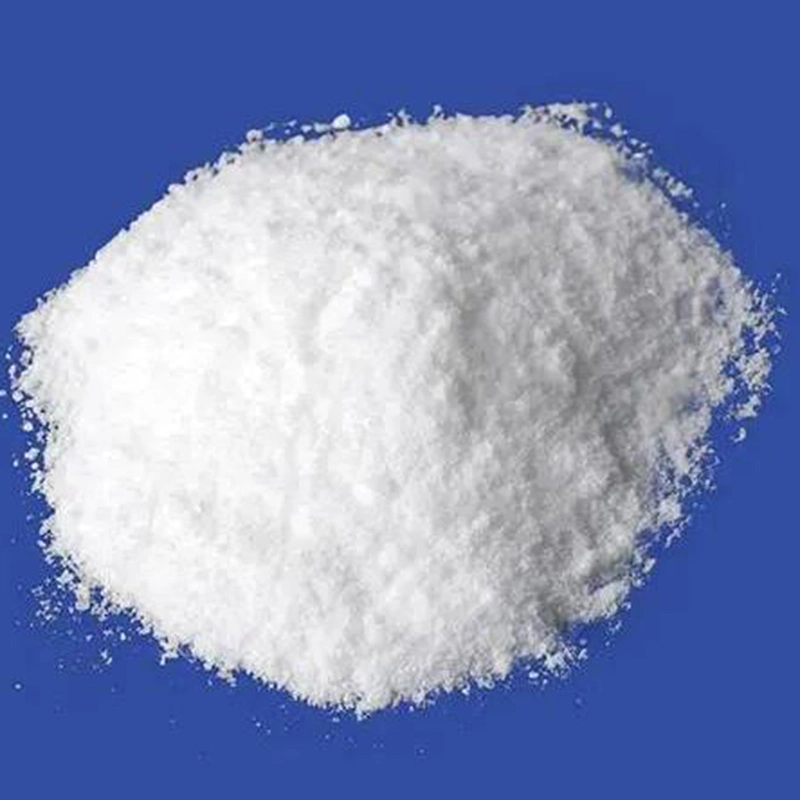
Hydroquinone is a critical pharmaceutical raw material widely supplied to API factories and pharmaceutical R&D labs globally. Our factory produces high purity pharmaceutical raw material that meets strict pharmacopoeial standards, supporting stable bulk orders and custom packaging for pharma manufacturers. If you are sourcing reliable Hydroquinone for pharmaceutical formulation development, our cGMP-compliant production line delivers consistent batch quality for your projects.
1. Strict Quality Control for High Purity Hydroquinone
Quality consistency is the top priority for pharmaceutical raw material procurement. Our Hydroquinone is manufactured under standardized purification processes, with purity exceeding 99.0% and full test reports including melting point, heavy metal limits and residue inspection. Every batch undergoes laboratory verification before shipment to match USP and EP specifications. Impurity control is tightly managed to avoid cross-contamination, a key requirement for downstream pharmaceutical synthesis. Customers can obtain full CoA, SDS and technical documents for registration and audit use. This rigorous quality system ensures that the high purity pharmaceutical raw material performs stably in your formulation trials and mass production.
2. Stable Supply Chain & Flexible Bulk Delivery
Many pharma developers struggle with unstable raw material lead times and fluctuating prices. As a direct manufacturer, we maintain sufficient inventory of Hydroquinone to handle small R&D trial orders and large-scale bulk shipments. We offer multiple packaging options and professional light-shield packing to protect the product from degradation during transit. Our logistics team arranges safe transport for this sensitive chemical worldwide. Whether you need trial samples or ton-level supply, we can customize delivery schedules to fit your production timeline. Our end-to-end supply model cuts intermediate costs and guarantees reliable availability of your pharmaceutical raw material.
3. Technical Support for Pharmaceutical Formulation Research
Working with a raw material supplier that understands pharma requirements accelerates your R&D progress. Our technical team provides professional guidance on proper storage, handling and compatibility of Hydroquinone. The product must be sealed and stored away from light and oxidants to retain its chemical properties. We can share technical data to assist your formulation design and stability testing. Our team responds quickly to technical inquiries and batch data requests. Partnering with us means you get not only high purity pharmaceutical raw material, but also dedicated technical backup to reduce risks in your pharmaceutical development cycle.
In summary, selecting a trusted source of Hydroquinone helps pharmaceutical manufacturers maintain stable production and meet global regulatory requirements. Our integrated manufacturing, strict QC and responsive service make us a preferred supplier of high purity pharmaceutical raw material for pharma clients across the world.
If you have any needs, please contact us via email to obtain a free quotation.